Providing custom chemical compounds engineered for absolute purity, reactivity, and application safety.
How precise molecular synthesis drives concrete performance, structural durability, and accelerating properties.
Within modern civil engineering and high-performance infrastructure projects, the modification of cementitious systems is vital. The chemical compound selection directly defines structural lifespan, set times, early strength development, and environmental resistance. Nitrate chemistry stands at the focal point of this technical category.
Calcium Nitrate, for instance, serves as an active set accelerator. By introducing active Ca2+ ions, it expedites the hydration of tricalcium silicate (C3S), yielding accelerated formation of calcium silicate hydrate (C-S-H) gel. This allows cold-weather concreting down to freezing temperatures without relying on chloride-based accelerants, which trigger internal reinforcement corrosion.
Simultaneously, Sodium Nitrate functions effectively as a structural corrosion inhibitor and set regulator. For companies sourcing OEM construction chemicals, obtaining industrial-grade salts with customized particle sizing and ultra-low heavy metal concentrations is critical for keeping formulations stable inside commercial admixtures.
To produce highly reliable chemical derivatives, a manufacturer must control the foundation of the reaction chain: Nitric Acid (HNO3). Uncompromising control of concentrations, from dilute solutions to fuming phases, dictates the structural integrity and purity of the resulting metal nitrates.
Henan Yongchang Nitro Fertilizer’s journey from a dedicated local manufacturer to a globally trusted titan.
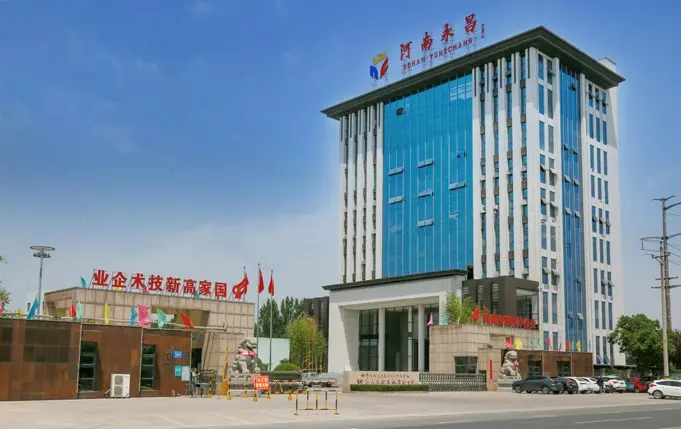
Founded in 1974, Henan Yongchang Nitro Fertilizer has evolved over half a century into a modern chemical industry leader. Our vertically integrated industrial matrix combines dilute and concentrated Nitric Acid production with downstream specialty derivatives.
Our integrated capacity encompasses 500,000 tons of dilute nitric acid, 300,000 tons of concentrated nitric acid, 300,000 tons of ammonium nitrate and structural derivatives, and 100,000 tons of custom chemical formulations. Through this comprehensive control, we insulate clients against supply fluctuations, guaranteeing chemical purity and batch uniformity across international operations.
How customized formulations solve specific geographic, geological, and operational challenges globally.
In cold climate regions (such as Northern Europe and Canada), construction schedules depend heavily on curing concrete at sub-zero temperatures. Incorporating custom-blended Calcium Nitrate prevents the freeze-thaw degradation of curing paste by accelerating cement hydration rates and lowering the freezing point of mixing water, maintaining scheduled structural strength gain.
In solar thermal installations located in arid, high-radiation regions, molten salt grade Sodium Nitrate and Potassium Nitrate act as the thermal energy transfer media. These materials must carry exceptionally high purity levels to prevent corrosion of heat exchangers and piping, maintaining continuous, clean energy output.
For ports, bridges, and off-shore structures constantly exposed to chloride-rich environments, our customized chemical blends containing Nitrates provide excellent anodic protection. By creating a stable passivation layer on the steel rebar, these chemicals prevent structural steel degradation, reducing long-term lifecycle maintenance expenses.
Evaluating shifting demands, supply chain risks, and technical performance expectations in international commerce.
The industrial landscape for construction chemicals is undergoing structural change. Real estate expansion, major transport infrastructure, and rapid industrialization in emerging markets are generating continuous demand for advanced cementitious additives.
At the same time, environmental safety requirements (such as limiting the use of formaldehyde, ammonia, and VOCs) are compelling developers to choose cleaner, mineral-based formulations. This shift reinforces the value of premium, high-purity nitrates, which offer clean catalytic actions, predictable reaction profiles, and zero volatile outgassing. Developing strong partnerships with vertical suppliers helps buyers avoid regulatory delays and raw material price volatility.
Driving processing efficiency, intelligent factory execution, and environmental sustainability.

Our proprietary Dual-Pressure Nitric Acid Process utilizes advanced catalytic absorption, lowering catalyst consumption while boosting energy recovery. This maintains our ranking among the world's most resource-efficient chemical synthesis pipelines.

By engineering advanced nitrogen-phosphorus delayed-release matrices, we improve crop nutrient absorption. In construction concrete, these same molecular control technologies permit customized, delayed hydration rates in commercial admixtures.

With an investment in digital factory infrastructure and automated quality monitoring, we are optimizing operations to achieve a 30% reduction in carbon footprint across our entire raw material synthesis and product packaging processes.
Our digital-twin manufacturing facility will integrate real-time quality control arrays directly with global supply networks. Simultaneously, we are implementing green hydrogen technologies to produce zero-carbon ammonia feedstocks, laying the foundation for environmentally sustainable nitric acid production.
By blending advanced Chinese chemical manufacturing with global quality management systems, Henan Yongchang Nitro Fertilizer ensures that our partners receive reliable materials designed to meet the performance challenges of today and the strict environmental standards of tomorrow.
Ensuring operational reliability, consistent shipping timelines, and meeting strict international regulatory demands.
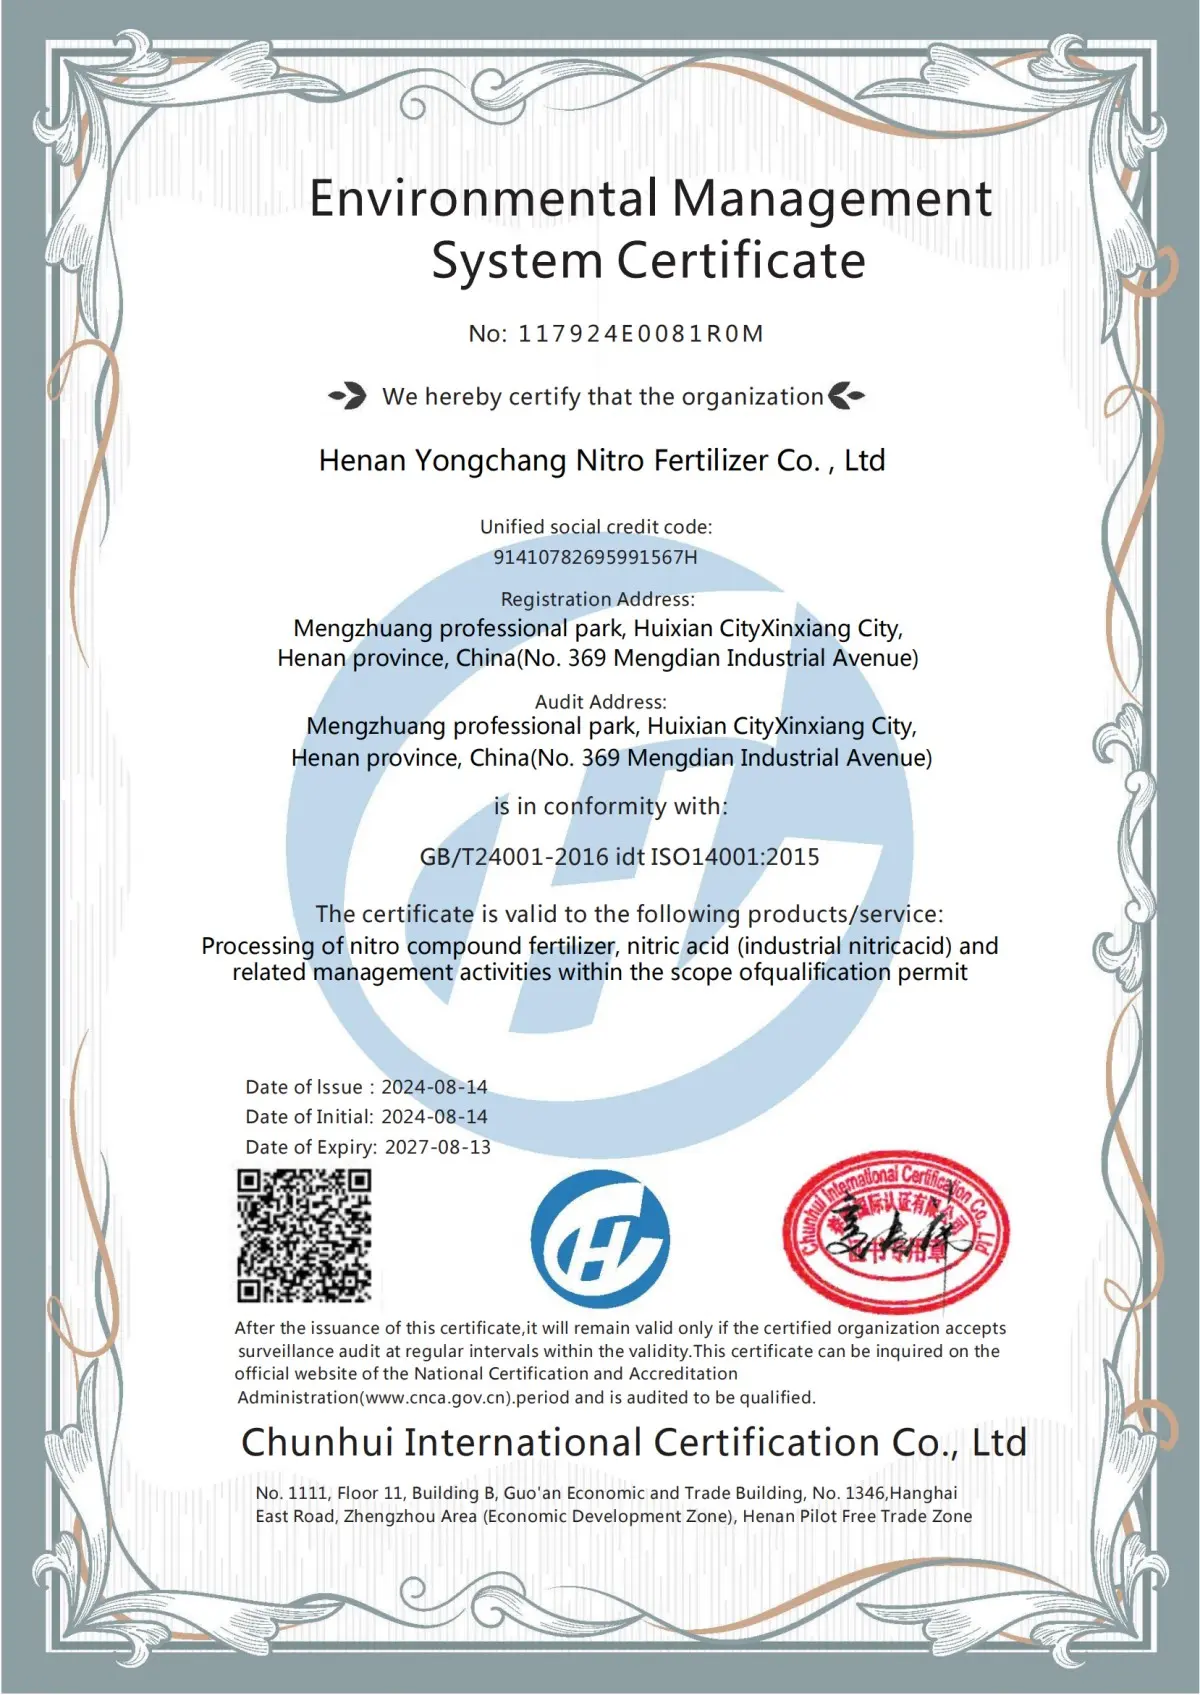
Exporting chemical materials worldwide requires strict adherence to international safety, purity, and environmental codes. Our facilities operate in compliance with ISO 9001 and ISO 14001, and we maintain certifications to support specific agricultural and industrial sectors, including FAMI-QS standards.
Additionally, our shipping and supply chain systems comply with REACH rules for European markets, together with IMDG and DOT packaging mandates for hazardous materials. Each batch comes with complete documentation, including certified COAs, technical specifications, and updated GHS Safety Data Sheets (SDS), ensuring smooth customs clearance and regulatory compliance at the destination port.
Operating from Central China’s chemical processing hubs, we benefit from reliable raw material access, directly integrating upstream ammonia production with downstream catalytic synthesis. This complete vertical control minimizes cost volatility and keeps production lines running smoothly during global supply disruptions.
Our transport logistics team integrates rail, barge, and ocean freight networks, connecting our manufacturing sites directly to major Chinese ports like Qingdao, Tianjin, and Shanghai. This versatile logistics setup minimizes overland transport delays and maintains stable product delivery timelines for our global customers.
From custom chemical formulations to local regulatory assistance, we provide tailored support for global projects.
We tailor nitrate purity levels, solid particle distributions, and aqueous concentrations to meet our clients' specific production processes and manufacturing targets.
We support clients with specialized compliance document packets, including REACH declarations, custom CAS registry filings, and country-specific GHS labels.
We offer diverse cargo packaging solutions, including robust bulk bags, heat-sealed bags, and insulated fluid containers, optimizing transit stability and unloading efficiency.
Technical answers to common questions about our products, manufacturing processes, and shipping capabilities.
Calcium Nitrate acts as a non-corrosive, non-chloride set accelerator. It releases calcium ions that accelerate the hydration of tricalcium silicate (C3S), cutting down initial set times and promoting rapid strength development. This is particularly valuable for cold-weather construction projects where concrete must gain early strength before freezing temperatures set in.
We maintain stable chemical properties by using our advanced, automated Dual-Pressure Nitric Acid process. Our quality assurance team uses online chromatography and laser analysis at every stage, verifying that every batch meets our strict purity standards from raw materials to final packaging.
Yes. We offer customized packaging options, including moisture-resistant polythene bags, UV-stable outer wrapping, and heavy-duty, heat-sealed IBC totes. These containers protect our products from humidity and heat during transit, ensuring they arrive at your facility in optimal condition.
Our molten salt grade Sodium Nitrate is produced to have a purity level of 99.8% or higher. We keep iron, chloride, and carbonate impurities to a minimum, helping prevent corrosion and maintain thermal efficiency in solar thermal storage systems and high-temperature heat transfer applications.
Targeted solutions designed to support modern agriculture, industrial manufacturing, and advanced chemical synthesis.
 Nitro Fertilizer